+8615061447755
Sand, heat and rock change the physics of a foundation job. On a temperate farmland site a crew can run a full 10–12 hour shift with a standard hydraulic ram; in a hot arid PV site, 45–50 °C ambient air, 60–70 °C surface temperature, abrasive airborne dust, and loose wind-blown sand over weathered rock cut the productive window to 6–8 hours and derate output by roughly 15–25%. Most failed desert schedules trace back to one mistake: specifying a solar farm piling platform from a temperate-climate catalog. This guide sets out seven installation challenges specific to desert solar farms, the quantified design ranges engineers use to handle each one, and the equipment configuration that survives a full season. All figures below are typical engineering ranges for utility-scale PV work in hot, arid regions — final values must come from the site geotechnical report and the machine's approved configuration sheet.
The seven challenges and their standard countermeasures are: (1) extreme heat — 45–50 °C ambient and 60–70 °C ground surface push hydraulic oil toward its 80–90 °C limit, so upsize the oil cooler 30–50% and stop work between 11:00 and 15:00; (2) airborne dust — shorten air-filter service from 250 h to 50–100 h and add cyclone pre-cleaners; (3) loose dune sand — bearing capacity below 50 kPa demands a tracked chassis at 35–55 kPa ground pressure; (4) weathered rock below the sand — drill 90–152 mm rock sockets 3–8 m deep with down-the-hole equipment; (5) wind uplift — increase embedment 0.3–0.8 m beyond the standard 1.5–3.5 m; (6) coating and corrosion — specify 65–85 µm hot-dip galvanizing or zinc-aluminium-magnesium; (7) water scarcity — use dry dust collection and air-flush drilling instead of wet suppression.
Rule of thumb: desert work is won or lost on cooling, filtration and ground pressure — not on impact energy. Specify those three first, then everything else follows from the geotechnical report.
|
45–50 °C
Typical peak summer ambient, hot arid PV sites
|
35–55 kPa
Tracked chassis ground pressure for loose dune sand
|
90–152 mm
Typical bore range for a grouted rock socket
|
15–25%
Typical output derate from heat stops and dust service
|
Use this table as the first page of the method statement. The benchmark column is what a designer needs to see in the geotechnical and meteorological data before a machine is selected; the fix column is what the machine and the crew must then deliver. Figures are typical engineering ranges for hot arid utility-scale PV sites, not universal constants.
| # | Challenge | Quantified benchmark | Practical fix |
|---|---|---|---|
| 1 | Extreme ambient and surface heat | 45–50 °C air; 60–70 °C surface; oil limit 80–90 °C | Cooler upsize 30–50%; midday stop 11:00–15:00 |
| 2 | Abrasive airborne dust | Filter interval 250 h → 50–100 h | Cyclone pre-cleaner, sealed electrics, daily blow-down |
| 3 | Loose wind-blown sand | Bearing capacity <50 kPa; dune layer 2–8 m | Tracks at 35–55 kPa; bog mats on access routes |
| 4 | Weathered rock beneath the sand | 90–152 mm bore; 3–8 m socket depth | Down-the-hole drilling plus grouted post |
| 5 | Wind uplift on shallow posts | 1.5–3.5 m standard embedment; +0.3–0.8 m for uplift | Deeper drive or socket; pull-out test on trial piles |
| 6 | Coating breakdown and saline dust | 65–85 µm hot-dip galvanizing baseline | Zinc-aluminium-magnesium or duplex coating in coastal desert |
| 7 | Water scarcity for suppression and curing | Wet methods can consume 0.5–2 m³ per 100 piles | Air-flush drilling, dry collector, pre-mixed grout |
Hydraulic oil is the first component to complain. Most mobile hydraulic systems are designed around a continuous oil temperature ceiling of 80–90 °C; once ambient air sits at 45–50 °C and the sun heats steel surfaces to 60–70 °C, a standard cooler has very little thermal headroom left. Oil viscosity falls, volumetric efficiency drops, seal life shortens, and the machine's down-force and cycle time both drift. The usual engineering response is a 30–50% larger oil cooler, a high-VI hydraulic oil grade approved for the ambient range, heat-shielded hose routing near the power pack, and a radiator core sized for the reduced air density. Ask the manufacturer for the approved ambient temperature range in writing — a machine rated to 40 °C is not a desert machine.
Operationally, the fix is scheduling rather than hardware. Crews on hot arid sites commonly work two windows — roughly 05:00–11:00 and 15:00–19:00 — giving 6–8 productive hours instead of 10–12, with the midday break also used for filter service and refuelling. Plan for a 15–25% seasonal output derate in the programme and price it into the cost per post; pretending the derate does not exist is what turns a nine-month foundation package into a twelve-month one. Cab air conditioning, shaded fuel storage, and tyre or track pressure checks in the cool of the morning are small details with an outsized effect on uptime.
Fine quartz dust behaves like lapping compound. On a clean site, a two-stage engine air filter might be serviced every 250 hours; in a windy desert season the same element can load up in 50–100 hours, and a clogged intake quietly costs power and fuel while a split element destroys the engine. A cyclone or ejector-type pre-cleaner ahead of the main filter, a restriction indicator visible from the cab, and a daily blow-down routine are the minimum. The same logic applies everywhere else: cylinder rod wipers and seal kits, track pins and bushings, radiator fins, electrical connectors at IP-rated enclosures, and the cooling fan screen. Specify a sealed, positively pressurized cab and confirm the machine's electrical connectors are rated for dust ingress, not just splash water.
Dust also changes the maintenance economics. Budget shorter service intervals and a larger on-site consumables stock than a temperate project would need — filters, wipers, seals, and hydraulic oil are cheap compared with a derated machine waiting three weeks for a courier. A factory that supplies a desert-specific spares kit with the machine, rather than a generic one, has usually done this before.
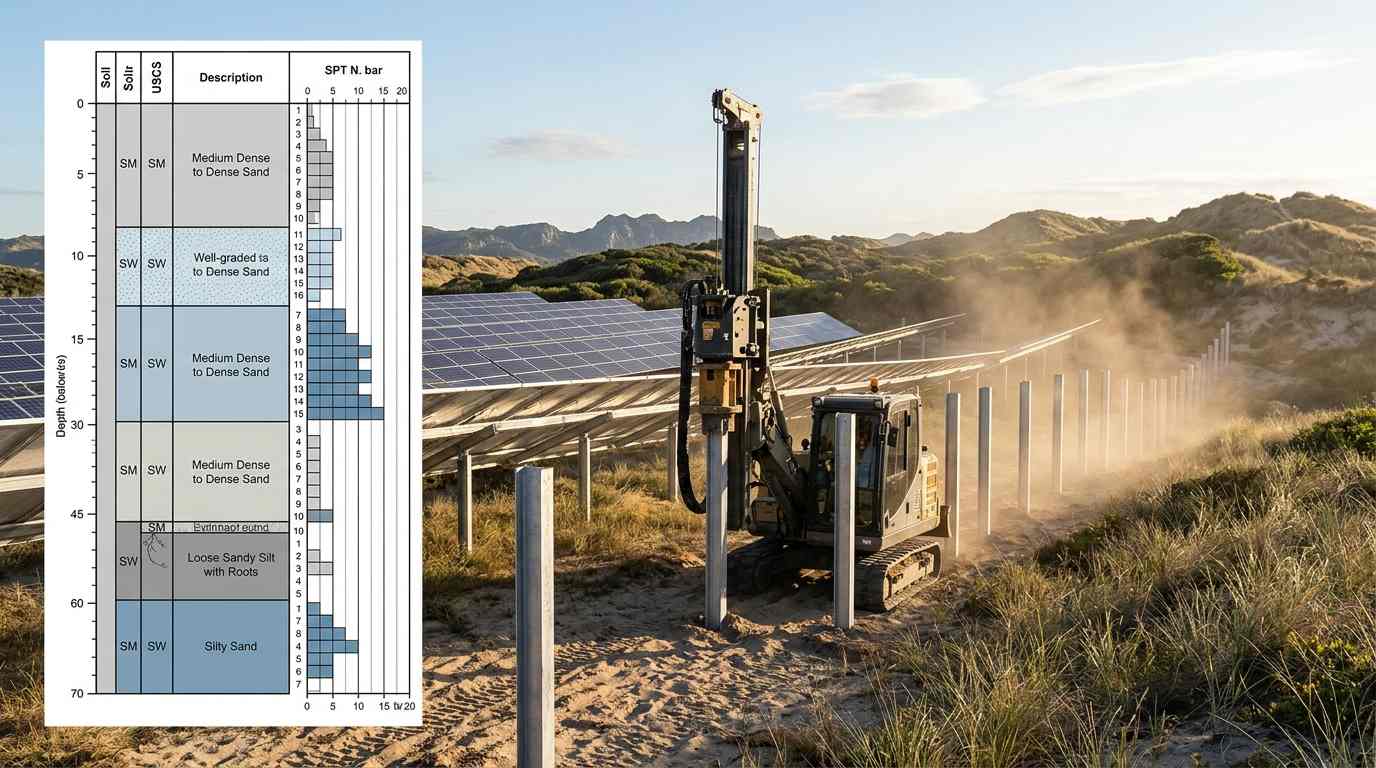
Wind-blown sand layers commonly run 2–8 m thick, with loose zones below 50 kPa bearing capacity and denser layers in the 60–120 kPa band. A wheeled unit that works perfectly on graded farmland will sink and spin here, which is why a tracked chassis at 35–55 kPa ground pressure is the default for dune-side work. Wide grouser shoes, bog mats on the access routes, and a low centre of gravity matter as much as raw power. Survey control needs attention too: on shifting sand, set out with GNSS to ±10–20 mm and re-check alignment frequently, because a post driven 1–2° out of vertical across a 3 m embedment can miss the module rail tolerance entirely.
Desert sites are rarely uniform: a project can run loose dune sand in one block and weathered limestone or sandstone in the next. Where a driven post meets refusal, the standard answer is a drilled and grouted rock socket — typically a 90–152 mm bore taken 3–8 m into competent rock, with the steel post grouted in. That means a down-the-hole drill for rock sockets on the same job as the ram, supplied by an air compressor in the 0.7–1.2 MPa / 8–12 m³/min class. Because water is scarce, air-flush drilling with a dry dust collector is preferred over wet flushing; note that compressor discharge temperature rises 10–15 °C above a temperate baseline in this ambient, so its cooling package needs the same scrutiny as the piling rig's.
This is the strongest argument for a multi-function platform. A 3-in-1 chassis that switches between ram driving, down-the-hole drilling, and auger work lets the crew follow the geology block by block without a second mobilisation — often the difference between one machine on site for the season and two machines each idle half the time. Ask the supplier to demonstrate the changeover on a video call and confirm the mast, hydraulic flow, and compressor interface support all three attachments.
| Ground condition | Recommended method | Typical parameters | Key watch-out |
|---|---|---|---|
| Loose dune sand, <50 kPa | Tracked ram driving with bog mats | Ground pressure 35–55 kPa; embedment 2.5–4.3 m | Flotation and verticality control |
| Dense sand / gravel, 60–120 kPa | Standard ram driving | 8–25 kJ impact energy; 76–114 mm posts | Check refusal on gravel lenses |
| Weathered rock, hardpan | Down-the-hole drilling + grouted post | 90–152 mm bore; 3–8 m socket; 0.7–1.2 MPa air | Dry dust collection, grout cure time |
| Cohesive or gypsiferous layer | Auger drilling | Bore matched to post + 20–40 mm annulus | Hole collapse, sulphate attack on grout |
Open desert terrain offers little wind shelter, and module arrays behave like aerofoils. Where a temperate design uses 1.5–3.5 m of embedment for a 76–114 mm post with 3–6 mm wall thickness, an exposed dune-side block is commonly pushed 0.3–0.8 m deeper, or into a grouted socket — and the design should be validated with pull-out tests on trial piles before full production. Coating is the other long-term variable: 65–85 µm hot-dip galvanizing is the usual baseline, upgraded to zinc-aluminium-magnesium or a duplex system where saline dust or coastal humidity is present. Any concrete used for sockets or pads should be placed below 30–35 °C with a curing regime that accounts for rapid moisture loss; high-temperature placement without wet curing loses a significant share of specified strength.
Below is the specification delta to send to a manufacturer when the site is hot and arid. Every line is a checkable item, and every one is cheaper to specify before production than to retrofit in the field. Ranges are typical engineering practice; confirm against the machine's approved configuration sheet.
| Subsystem | Temperate standard | Hot arid specification | Why |
|---|---|---|---|
| Hydraulic cooling | Standard oil cooler, 40 °C rating | 30–50% larger core; 50 °C ambient rating | Keeps oil under the 80–90 °C ceiling |
| Engine air intake | Two-stage filter, 250 h service | Cyclone pre-cleaner; 50–100 h service; restriction gauge | Fine quartz dust loads elements 3–5× faster |
| Undercarriage | Narrow shoes; wheeled option common | Wide grouser tracks at 35–55 kPa; sealed pins | Flotation on <50 kPa sand; abrasion life |
| Hydraulic fluid and hoses | Standard VG grade | High-VI oil; heat-shielded hose routing | Viscosity stability and hose life at 60–70 °C surface |
| Electrical and cab | Splash-rated connectors | Dust-rated enclosures; pressurized, air-conditioned cab | Connector failures and operator heat stress |
| Drilling attachments | Ram only | Ram + DTH + auger; dry dust collector; 8–12 m³/min air | Mixed geology, zero-water operation |
| Spares kit | 3–5% of unit price, generic | Desert kit: extra filters, wipers, seals, cooler belts | Shorter service intervals, remote site logistics |
1. Confirm the ground model. Read the borehole logs block by block — sand depth, bearing capacity, rock head level, and any gypsiferous layer. This decides method and embedment for every section.
2. Set out and record. GNSS control to ±10–20 mm, with daily re-checks on shifting sand; log every pile ID against its design depth.
3. Drive trial piles. Run 5–10 test posts per geology block, measure refusal and verticality, and validate pull-out resistance before production starts.
4. Prep the machine for heat. Verify the cooler upsize, oil grade, pre-cleaner, and filter stock; record baseline oil temperature during the first morning shift.
5. Work the cool windows. Two shifts around the 11:00–15:00 stop; use the break for filter service, refuelling, and radiator blow-down.
6. Switch method at refusal. Where ram driving stalls, change to down-the-hole drilling and a grouted socket rather than over-driving and bending the post.
7. Close out with QC records. Capture depth, verticality, pull-out results, coating thickness, and grout batch data per pile for the handover file.
1. Specifying for average ground. A single sand-layer assumption fails the moment the rock head rises; plan the method change in the contract, not on site.
2. Ignoring the ambient rating. A machine certified for 40 °C will spend a desert summer in thermal derate — get the approved temperature range in writing.
3. Keeping temperate filter intervals. A 250 h service schedule in quartz dust is an engine claim waiting to happen.
4. Pricing on a 10–12 hour shift. With a 6–8 hour productive window and a 15–25% derate, the cost per post changes — tender with the real programme.
5. Assuming water is available. Wet suppression and conventional curing can consume 0.5–2 m³ per 100 piles; design dry methods in from the start.
A manufacturer or OEM factory that has actually delivered into hot arid regions will answer four questions with specifics rather than adjectives: what is the approved continuous ambient temperature for this exact model; what cooling and filtration options are fitted and how much capacity do they add; can the platform switch between ram, DTH and auger without a second machine; and what does the desert spares kit contain and for how many operating hours. Ask for the configuration sheet, the CE and ISO9001 documents matching the offered model, and a reference project in a comparable climate. A wholesale supplier who cannot produce a high-temperature configuration in writing is quoting a temperate machine with a desert paint job.
Also confirm the supporting scope: compressor sizing for the drilling attachment, dry dust collection rather than wet suppression, coating specification for the posts, and on-site commissioning or remote engineering support in your time zone. Site-road and perimeter fencing work on these projects often runs on the same mobilisation schedule, so a supplier able to cover the full equipment scope — piling, rock drilling, compressed air, and roadside barrier work — reduces both freight and coordination overhead. Factory-direct buyers should lock these items into the configuration annex before the deposit, when changes are still cheap.
Can a standard piling machine work in 45–50 °C desert heat?
Not without derating. Standard hydraulic packages are usually designed around a 40 °C ambient and an 80–90 °C continuous oil temperature ceiling; at 45–50 °C ambient the cooler has little headroom left. Specify a 30–50% larger oil cooler, a high-VI hydraulic oil approved for the range, heat-shielded hoses, and a two-window shift plan around the midday stop. Ask for the approved ambient rating in the machine documentation.
How deep should PV posts be driven in loose desert sand?
Typical utility-scale posts are 76–114 mm in diameter with 3–6 mm walls and 1.5–3.5 m embedment on temperate ground. On exposed dune-side blocks with high wind uplift, designers commonly add 0.3–0.8 m, taking total embedment to roughly 2.5–4.3 m, and validate the design with pull-out tests on trial piles. Final depth must come from the geotechnical and wind-load calculations, not a catalog figure.
What is the right method when sand sits over weathered rock?
Plan for two methods on one site. Ram driving handles the sand; where the rock head rises, switch to a drilled and grouted socket — typically 90–152 mm bore, 3–8 m into competent rock — using down-the-hole drilling with an air compressor in the 0.7–1.2 MPa / 8–12 m³/min class. A 3-in-1 ram/DTH/auger platform avoids mobilising a second machine for the changeover.
How does dust change the maintenance schedule?
Expect to shorten engine air-filter service from a typical 250 hours to 50–100 hours, add a cyclone pre-cleaner and a restriction indicator, and blow down radiator fins and filter housings daily. Specify dust-rated electrical enclosures, sealed track pins, and quality rod wipers, and ship a desert spares kit with extra filters, seals, and cooler belts. Budget a 15–25% seasonal output derate for heat stops and the extra service time.


+8615061447755
 شبكة IPv6 المدعومة
Our hours
سواء كان ذلك يوم عطلة أو مهرجان، سيكون لدينا شخص لاستقبالك على مدار 24 ساعة في اليوم والرد عليك في أقصر وقت.
Hi! Click one of our members below to chat on